What Is the Best Ventilation System for a Poultry Cage Farm in Nigeria?
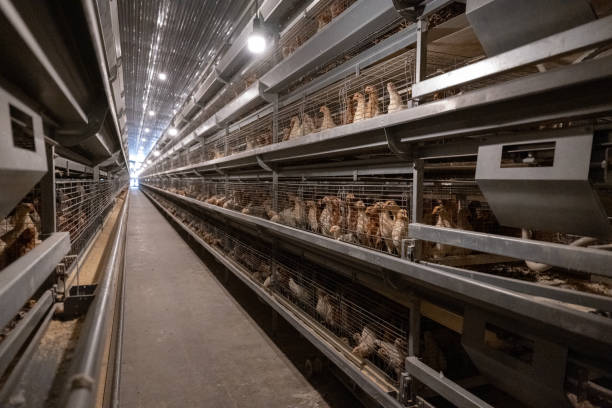
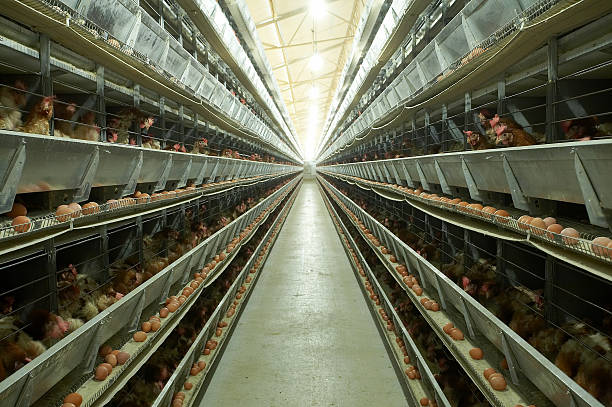
In large-scale poultry farming, proper ventilation is crucial for ensuring the health, productivity, and overall well-being of chickens. For a poultry cage farm housing 100,000 chickens in Nigeria, choosing the right ventilation system can significantly improve air quality, reduce disease risks, and enhance egg and meat production.
The Importance of Ventilation in Poultry Farming
Effective ventilation in poultry farming serves multiple purposes:
- Ammonia and CO2 Removal: Chickens produce a large amount of ammonia and carbon dioxide, which can be harmful if not properly removed.
- Temperature Regulation: Nigeria’s warm climate requires a system that can keep the flock cool and prevent heat stress.
- Humidity Control: Proper ventilation prevents excess moisture buildup, reducing the risk of bacterial and fungal diseases.
- Improved Oxygen Supply: Ensuring fresh air circulation optimizes growth and egg-laying efficiency.

Best Ventilation System for Large-Scale Poultry Farms
For a poultry farm with 100,000 birds, tunnel ventilation is the best solution. Tunnel ventilation is a high-efficiency system that creates a consistent airflow through the poultry house, ensuring proper temperature control and air quality. The key components include:
- Exhaust Fans: Powerful fans placed at one end of the poultry house pull air through the system.
- Cooling Pads: Located at the opposite end, cooling pads lower the temperature as air passes through.
- Air Inlets: These ensure uniform air distribution and prevent dead zones.
- Automated Climate Control: Sensors adjust ventilation based on temperature and humidity levels.
Livi Poultry Equipment: The Best Choice for Automated Chicken Farming
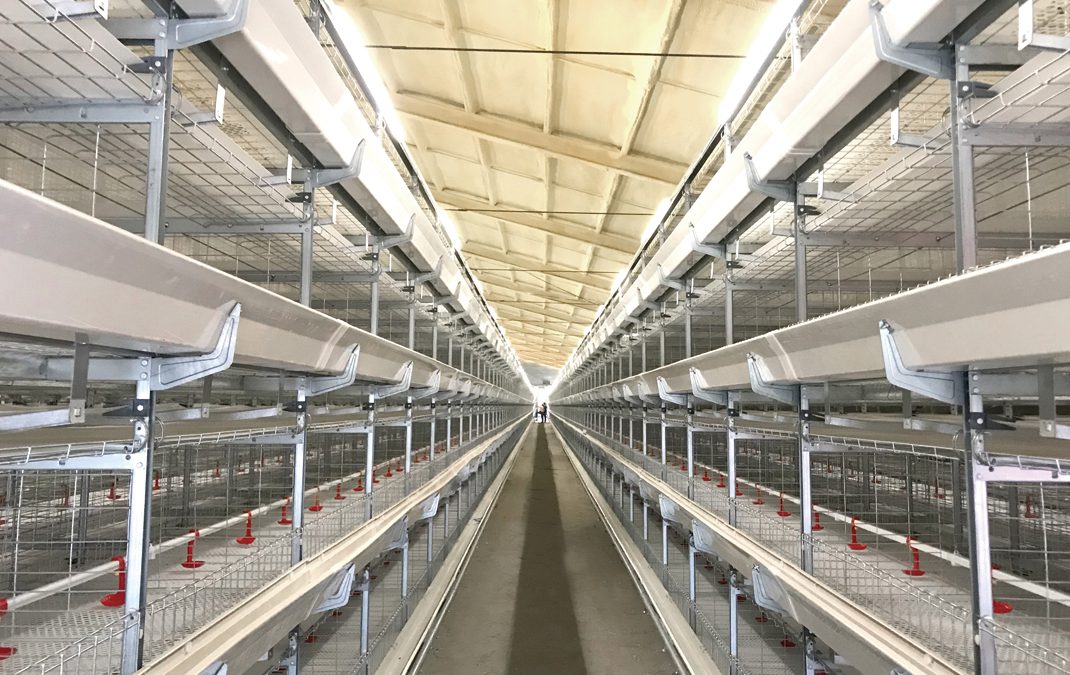
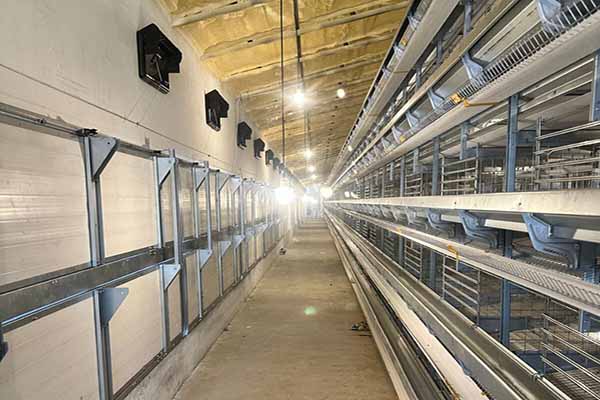
At Livi Machinery, we specialize in providing cutting-edge automated poultry cage systems and ventilation solutions designed to enhance productivity and efficiency in poultry farming. Our H-Type and A-Type Layer Cages, Broiler Cages, and Breeding Cages are designed for durability, high stocking density, and optimal airflow.
Advantages of Livi’s Poultry Farming Equipment
- Automated Ventilation Systems: Our systems ensure a constant supply of fresh air while maintaining the right temperature and humidity.
- High-Density Cage Systems: Designed to maximize space utilization while providing comfortable living conditions for birds.
- Automatic Feeding and Drinking Systems: Reduces labor costs and ensures uniform feed distribution.
- Waste Management Solutions: Our automated manure removal systems help maintain hygiene and reduce ammonia levels.
- Energy-Efficient Solutions: Designed to minimize electricity consumption, making poultry farming more sustainable and cost-effective.
Why Choose Livi Machinery?
- Proven Track Record: Trusted by poultry farmers worldwide.
- Customizable Solutions: We tailor our equipment to meet your farm’s specific needs.
- After-Sales Support: Comprehensive training and technical assistance to ensure smooth operation.
- Competitive Pricing: High-quality equipment at affordable prices.
Conclusion
For poultry farmers in Nigeria operating large-scale farms, tunnel ventilation combined with Livi’s automated poultry farming equipment is the ideal solution. It ensures optimal air quality, improves productivity, and enhances the overall efficiency of poultry farming operations.
Invest in Livi Machinery’s automated poultry cage systems today and take your poultry farm to the next level. Contact us now for a customized solution that fits your needs!