Chicken Cage Supplier for 15,000 Layers – Livi Machinery
Chicken Cage Supplier for 15,000 Layers – Livi Machinery
Running a large-scale poultry farm with 15,000 laying hens is no small task. From feeding efficiency to egg production consistency, every detail matters — and the foundation of your entire operation starts with the right chicken cage system. As your trusted chicken cage supplier for 15,000 layers, Livi Machinery has been delivering tailored, high-performance solutions since 2012, helping farmers worldwide achieve better productivity, healthier flocks, and smoother daily operations.
We understand that choosing a supplier for such a large setup requires confidence in quality, scalability, and long-term support. That’s why at Livi Machinery, we don’t just sell equipment — we partner with you from design to delivery, ensuring your facility runs efficiently from day one. Our systems are engineered for durability, optimized space usage, bird comfort, and labor-saving automation.
Whether you’re setting up a new farm or upgrading an existing one, our team will walk you through planning, customization, installation guidance, and after-sales service — all designed specifically for operations handling around 15,000 layer hens.
Why Choose Livi Machinery for Your 15,000-Layer Farm?
When it comes to selecting a chicken cage supplier for a project this big, experience and reliability matter most. At Livi Machinery, we’ve spent over a decade perfecting our designs by working directly with commercial farms across Asia, Africa, South America, and Eastern Europe. Our hands-on approach allows us to create solutions that aren’t just technically sound but practical on the ground.
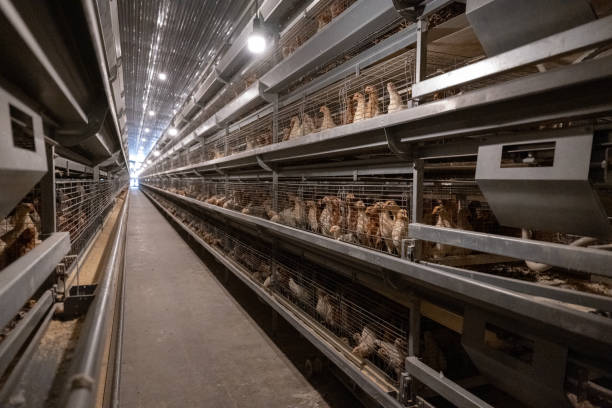
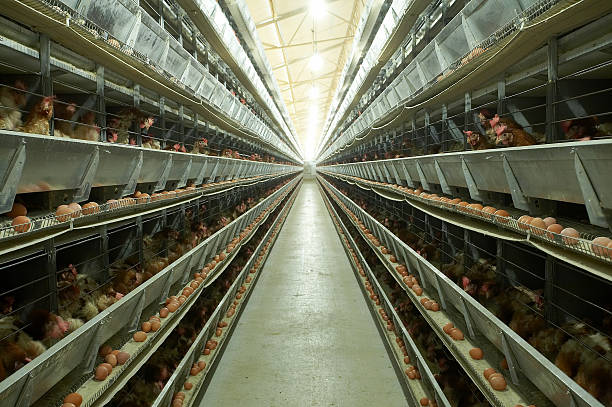
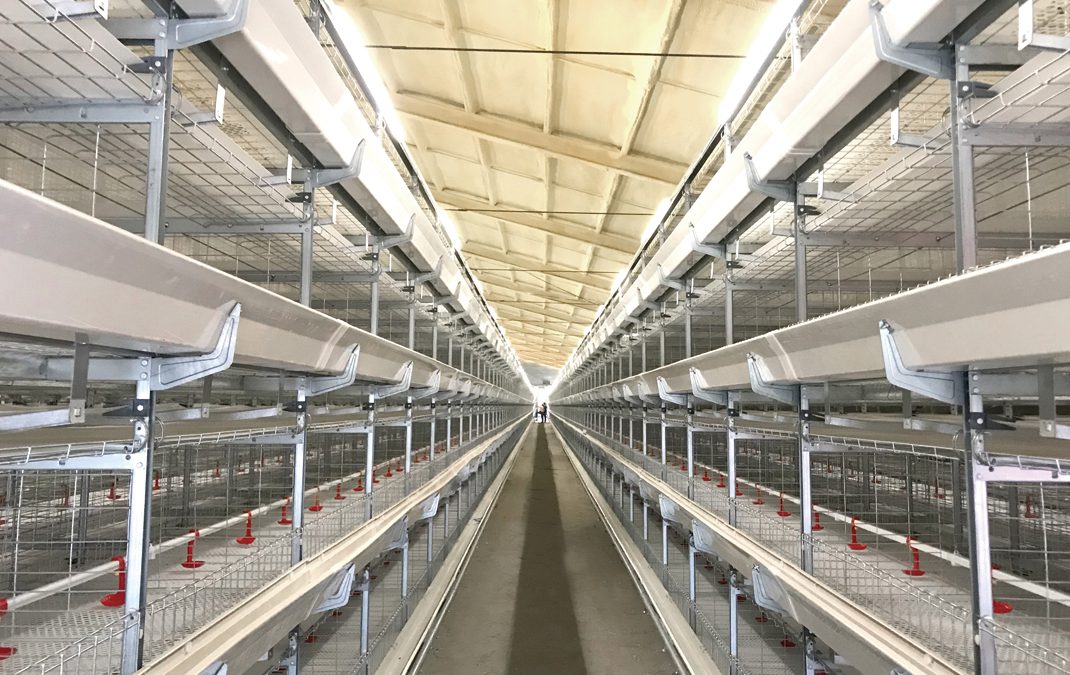
Our standard solution for 15,000 birds usually includes multi-tier A-frame or H-type battery cages laid out across multiple house sections. Depending on your barn size and local climate, we customize the layout to maximize capacity while maintaining airflow, ease of access, and waste removal efficiency. For example, a typical 15,000-layer setup might require three houses with 5,000 birds each, or one large well-ventilated building using automated feeding, watering, egg collection, and manure belt systems.
What sets us apart? First, our materials: hot-dipped galvanized steel ensures up to 15 years of rust-free performance, even under high humidity. Second, smart integration — our cages work seamlessly with automatic feeders, nipple drinkers, and conveyor belts so you can run the whole farm with minimal manual labor. Third, full pre-assembly testing before shipping guarantees fast installation upon arrival.
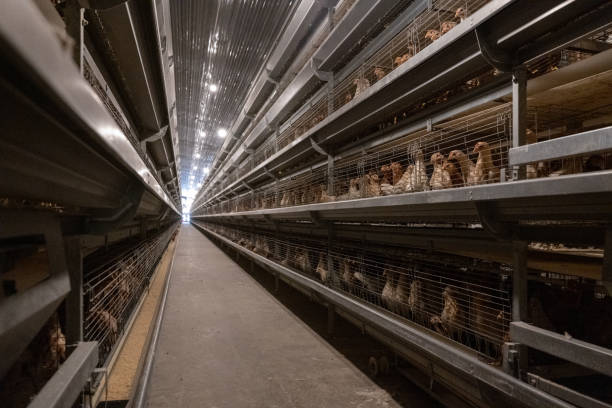
And because we manufacture everything in-house at our modern facility in Zhengzhou, China, we maintain strict control over cost, quality, and delivery timelines. No middlemen, no surprises.
Smart Features Built Into Every System
Modern layer farming isn’t just about housing birds — it’s about managing health, improving yields, and cutting operational costs. That’s why our cage systems come equipped with intelligent features designed to make your life easier.
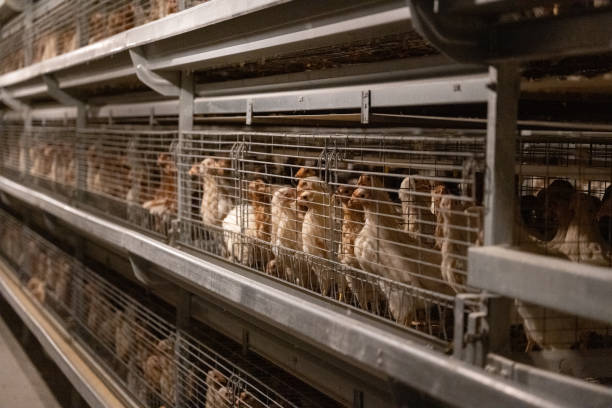
For starters, our nesting areas are angled correctly to encourage hens to lay in designated zones, which reduces floor eggs and improves cleanliness. The sloped bottom wires gently roll eggs toward collector belts, minimizing breakage and contamination. This feature alone can increase saleable egg recovery by up to 3%.
Second, we use UV-resistant plastic trays beneath each tier to catch droppings, reducing ammonia buildup and simplifying cleaning. These trays last longer than metal counterparts and don’t corrode — an important factor when dealing with thousands of birds producing waste daily.
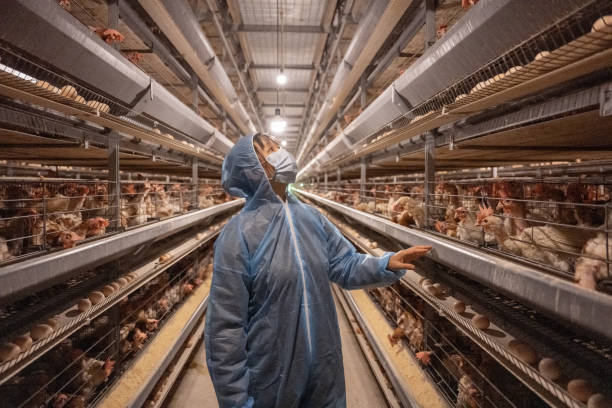
Third, our ventilation-compatible designs allow proper air circulation between levels, preventing heat stress during warmer months. In colder regions, we recommend side-curtain adjustments or insulated walls paired with mechanical fans, all factored into your initial plan.
Automation plays a huge role too. With optional upgrades, you can include auto-feed lines (chain or auger type), drinker line flushers, timed lighting controls, and centralized egg sorting stations. Many of our clients report saving 4–6 hours per day on routine tasks thanks to these integrations.
And don’t forget biosecurity. All components are easy to clean and disinfect between cycles. Our modular design means parts can be disassembled quickly if needed, helping prevent disease spread during flock turnover.
Over time, these small advantages add up — healthier birds, less labor, lower mortality rates, and higher profits.
From Blueprint to Barn: How We Deliver Results
You might have the perfect site picked out, or maybe you’re still finalizing land acquisition — either way, we start with listening. Our engineers will ask key questions: What’s your available barn size? Do you already have infrastructure like water supply or power connections? Are you aiming for fully manual or near-total automation?
Based on your answers, we generate a free preliminary layout showing pen arrangement, equipment placement, and recommended walkways. We calculate stocking density (usually 7–8 hens per square meter depending on local standards) and confirm how many tiers fit safely within your ceiling height.
Once approved, we move to manufacturing. Production takes 25–30 days, and we offer flexible shipping options via container load (FCL) or bulk vessel depending on destination. Each set arrives labeled, organized, and pre-packed to simplify assembly.
Need help installing? We provide detailed video tutorials, PDF manuals, and Zoom walkthroughs — plus, if required, we can dispatch a technician to supervise local workers. Clients in Nigeria, Bangladesh, and Peru have successfully installed their full 15,000-bird setups in under two weeks.
After commissioning, our support doesn’t end. We stay in touch for troubleshooting, spare part replacements (like broken egg belts or feeder chains), and future expansion advice. Think of us as your long-term partner in poultry success.
Ready to Scale Up Efficiently?
If you’re serious about building or upgrading a 15,000-layer operation with reliable, durable, and smart equipment, now is the time to connect with a proven industry leader. At Livi Machinery, we’ve helped hundreds of farmers just like you turn ambitious plans into profitable reality.
Before placing any order, let’s talk. Tell us about your goals, location, budget, and timeline — we’ll respond with a personalized plan including 3D layout, quote breakdown, production schedule, and ROI projections based on average egg output and labor savings.
Don’t leave your farm’s foundation to chance. Contact Livi Machinery today and get a free consultation from experts who’ve been solving real-world poultry challenges for more than a decade. Just leave your name, email, and phone number below, and we’ll reach out within 24 hours.
Let’s build something great together.