Large-Scale Battery Cage System for 120,000 Chickens
Large-Scale Battery Cage System for 120,000 Chickens
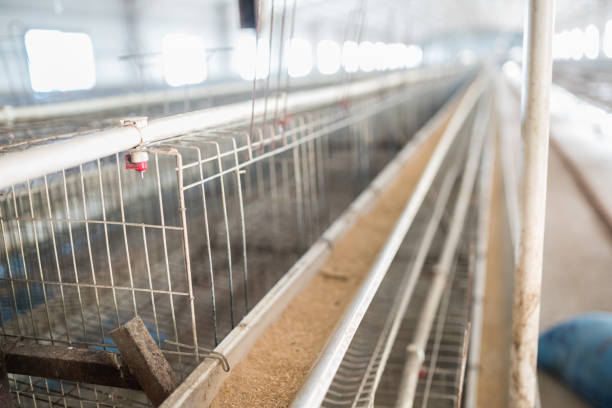
If you’re running or planning a large-scale commercial egg farm, investing in the right poultry housing system is absolutely crucial. For farms aiming to manage 120,000 chickens efficiently, a large-scale battery cage system isn’t just an option — it’s a smart business decision. At Livi Machinery, we’ve helped hundreds of poultry farmers across Asia, Africa, and South America scale up production using our customized, durable, and high-tech battery cage solutions. In this article, we’ll walk you through what a 120,000-chicken battery cage setup looks like, why it’s ideal for commercial operations, how to design it properly, and what makes our systems stand out from the crowd.
What Does a 120,000-Chicken Battery Cage Setup Look Like?
To handle 120,000 laying hens, you can’t simply pile cages on top of each other without careful planning. A well-designed system typically divides the flock into sections across multiple sheds or barns. Each barn usually holds between 20,000 and 30,000 birds, meaning your farm would need four to six fully equipped poultry houses.
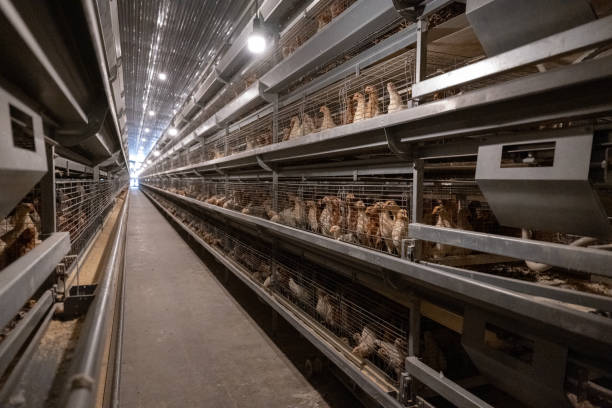
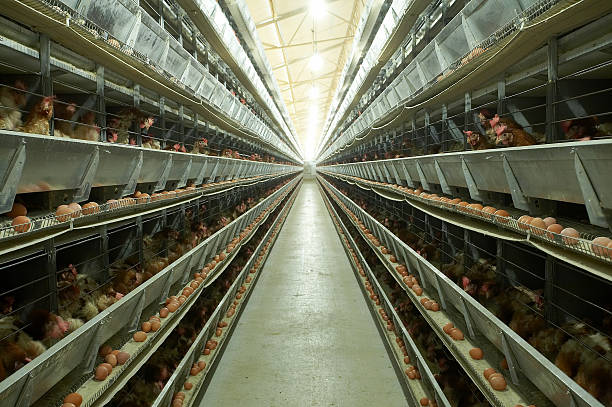
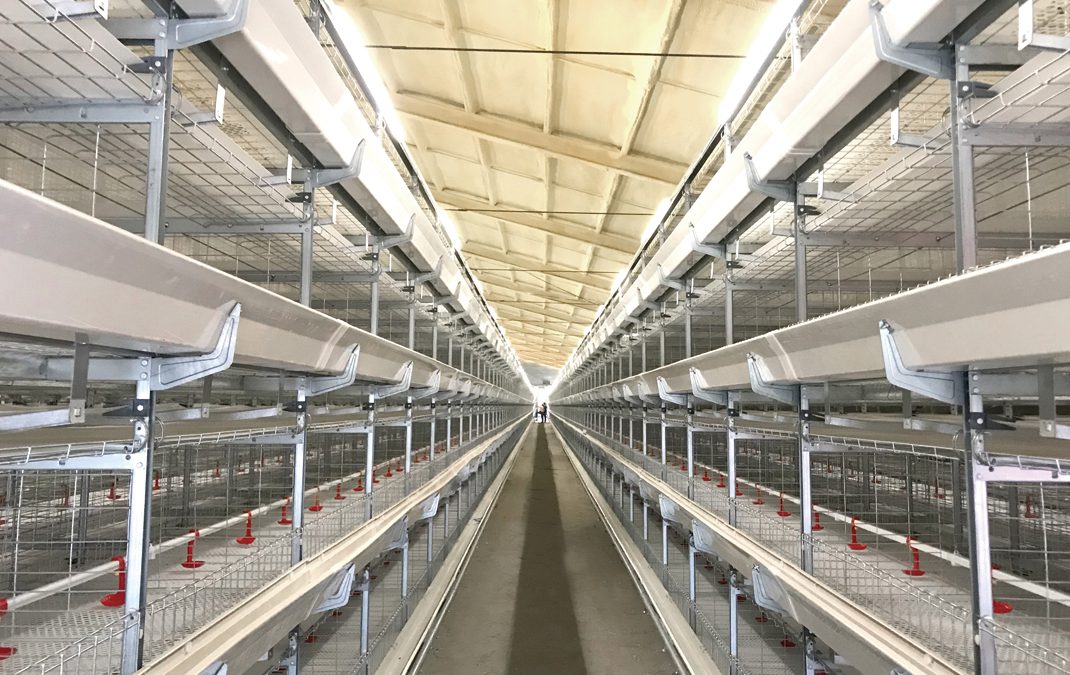
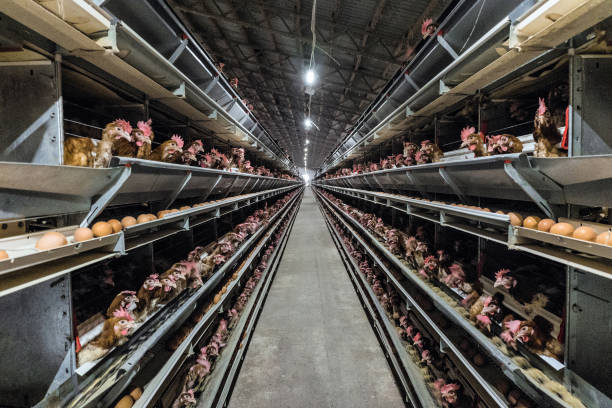
Each house uses a tiered battery cage configuration — generally ranging from 3 to 4 tiers high. This vertical design maximizes space and allows for automated feeding, watering, manure removal, and egg collection. With proper ventilation and climate control, one trained worker can manage thousands of birds per shift.
For example, a standard 4-tier A-frame battery cage system covers about 1.2 square meters per 85–90 hens. That means, with efficient space use, you’d need roughly 13,000 to 14,000 square meters (about 3–3.5 acres) of enclosed building space in total. Our engineers at Livi help clients optimize layout based on land size, local weather conditions, and future expansion plans so that every square foot counts.
These systems include automatic nipple drinkers, chain feeders, belt manure collectors, and egg belts that transport eggs directly to grading stations. All these components reduce labor costs, improve hygiene, and minimize stress on the birds — which translates directly into higher egg production and fewer diseases.
Why Choose a Battery Cage System for High-Density Farming?
You might be wondering: “Aren’t there alternatives like free-range or aviary systems?” Yes, there are — but when you’re working with 120,000 birds, consistency, efficiency, and biosecurity become non-negotiable factors. And that’s where battery cages truly shine.
Battery cages offer complete control over the hen’s environment. You decide the temperature, lighting schedule, airflow, and even meal timing. This precision leads to better feed conversion ratios and more predictable egg output — often exceeding 90% lay rates during peak production.
From a disease prevention standpoint, elevated cages keep hens off the ground, reducing contact with droppings and lowering the risk of parasites like mites or coccidiosis. Combined with automated manure belts that remove waste daily, your farm stays cleaner, healthier, and odor-free compared to deep-litter systems.
Labor savings are massive too. Instead of dozens of workers manually collecting eggs and cleaning floors, you’re looking at less than ten skilled technicians managing the entire complex — thanks to automation built into our Livi systems. Think about it: no more back-breaking labor, fewer injuries, lower staff turnover.
And let’s not forget scalability. If today you’re running 120,000 layers, tomorrow could be 200,000. Our modular battery cage units are easy to expand. Just add another row, another house, plug in the automation lines, and go.
Design & Customization: Building the Perfect Setup
No two farms are exactly alike — especially when dealing with different climates, power availability, and regulatory requirements. That’s why a cookie-cutter approach won’t work at this scale.
At Livi, we don’t just sell cages; we deliver turnkey solutions. When you order a 120,000-bird system, our team starts by analyzing your site — slope, soil type, wind patterns, water access, electricity supply, and local animal welfare regulations. Based on that data, we generate a detailed engineering plan including barn dimensions, cage arrangement, ventilation strategy, and automation specs.
We offer both galvanized steel and plastic-coated wire options depending on your region’s humidity levels. In tropical areas with high moisture, corrosion-resistant materials are essential for longevity. Our cages come with anti-rust treatment and can last over 15 years under normal conditions.
Custom features also matter. Need a double-decker egg collection belt because of narrow barn width? We can modify the design. Want solar-powered backup for feeders during blackouts? We integrate renewable energy compatibility. Interested in adding IoT sensors to monitor bird weight, temperature, or water usage in real-time? We partner with tech providers to bring smart farming to your doorstep.
Plus, we assist with installation training, spare parts inventory, and after-sales support — because installing thousands of cages across kilometers of wiring isn’t something you want to figure out alone.
One recent project in Nigeria involved setting up six identical poultry houses with full automation. By pre-assembling cage sections in our Zhengzhou factory and shipping them flat-packed, we cut on-site construction time by 40%. The client was operational within eight weeks and reached full production capacity in five months.
Why Farmers Trust Livi for Large Projects
Since 2012, Livi Machinery has specialized in building robust, intelligent poultry farming equipment tailored for commercial success. Our battery cage systems are used in over 30 countries, from cold Siberian regions to hot and humid Southeast Asian farms.
What sets us apart? It’s the combination of proven durability, innovation, and personalized service. Every component is tested rigorously before shipment. Our galvanization process exceeds international standards. And unlike generic suppliers, we take responsibility for performance — not just delivery.
Clients love our responsiveness. Whether you have questions about cage spacing, ventilation fan placement, or programming the controller box for nighttime dimming, our bilingual engineers respond fast — often within hours.
We also offer financing guidance and help connect buyers with trusted logistics partners who specialize in heavy machinery shipping. No need to worry about customs delays or damaged crates — we’ve navigated it all before.
If you’re serious about launching or upgrading a mega-layer farm, now is the time to talk. With rising global demand for eggs and protein, operating at scale gives you a huge competitive advantage. And with Livi as your partner, you won’t just survive the challenges — you’ll thrive.
Ready to build your dream farm? Share your project details — barn size, location, desired number of birds per house — and we’ll send you a free preliminary design and quote. Click below or send us an email. Let’s make your vision a reality.